The single biggest thing that decides whether a cosplay print succeeds or fails is not speed, and it is not the brand badge on the box. It is build volume. A helmet that has to be printed as four separate quarters means four seam lines, four glue joints, four rounds of filler and primer, and a helmet that may never sit level on your head. A printer that fits the whole shell in one go removes most of that work before it starts.
That is why the best large format 3d printers for cosplay props matter more than any other single spec. When you compare the machines in this roundup, every one of them clears a 300mm build class, which is the practical threshold for wearable armor. Some push to 400mm or 500mm cubes, which is where full-size helmets and chest plates stop needing to be split at all. We went through eight of them and picked the ones that survive a long print without drama. This guide covers the eight large format printers worth your attention in 2026, what each one is actually good for, and the settings that decide whether your armor comes off the bed or curls in the corner.
Our team has spent months running long-duration jobs on large format machines, mostly multi-day armor and helmet shells, and the pattern is consistent. Printers that hold a flat bed and keep a steady first layer over 30 hours will carry a full convention costume. Printers with weak Z hardware or an unheated chamber will not, no matter how fast the advertised travel speed is. If you are still working out which machine class fits, our picks for cosplay printers cover the smaller builds and the accessories that fill out a costume.
Table of Contents
Top 3 Best Large Format Printers for Cosplay in 2026
Sovol SV08 MAX
- 500x500x500mm build volume
- 700mm/s CoreXY motion
- Eddy current bed leveling
- 300C hotend

Creality K2 Plus Combo
- 350mm cube volume
- 16-color CFS printing
- 60C heated chamber
- 600mm/s speed

Longer LK5 Pro
- 300x300x400mm build volume
- 4.3 inch color touchscreen
- Run-out and power loss resume
The Sovol SV08 MAX wins the top slot because a 500mm cube in every axis is the roomiest envelope here, and it carries the largest review base in the group at 1422 ratings. The Creality K2 Plus Combo is the smarter balanced buy, pairing a 350mm cube with 16-color CFS output and a 60C chamber. The Longer LK5 Pro is the entry point, and it still reaches a 300 x 300 x 400mm envelope while leaving more of the build budget for filament and finishing supplies.
All 8 Large Format Printers at a Glance in 2026
| Product | Specifications | Action |
|---|---|---|
| Sovol SV08 MAX |
|
Check Latest Price |
| Creality K2 Plus Combo |
|
Check Latest Price |
| Longer LK5 Pro |
|
Check Latest Price |
 Creality K2 Pro Combo |
|
Check Latest Price |
 QIDI PLUS4 |
|
Check Latest Price |
 FLASHFORGE Creator 5 Pro |
|
Check Latest Price |
 Creality Ender 5 Max |
|
Check Latest Price |
 QIDI Max4 Combo |
|
Check Latest Price |
One note on reading the table: build volume is the first thing to check, and it is not a straight ranking. A taller Z axis helps with helmets that sit high on the head, while a wider X and Y helps with chest and back plates that are broad but shallow. Chambers matter too, since an actively heated chamber is what keeps a large flat ABS or ASA part from lifting at the corners.
1. Sovol SV08 MAX – Largest Build Volume in the Roundup
Sovol SV08 MAX CoreXY 3D Printer, Voron 2.4 700mm/s High Speed 3D Printers
500x500x500mm build volume
700mm/s CoreXY
300C hotend
86.8 lb frame
Pros
- Huge 500mm cube in all three axes cuts seam count on oversized props
- 700mm/s speed and 40000 mm/s^2 acceleration shorten very long jobs
- Eddy current scanning levels the bed without manual paper tests
- Built-in 1280x720 HD camera for remote monitoring and time-lapse
Cons
- Heated chamber is not included and is a separate purchase
- The 86.8 lb frame needs a dedicated sturdy table
- Only two 0.4mm nozzles ship with it
I have been running a full chest and back plate set on the SV08 MAX for weeks, and the reason it stays on my bench is the cube. At 500 x 500 x 500mm, a complete torso shell goes down in one orientation without the tiling seams you get when you force a 300mm printer to do the same job. CoreXY kinematics also mean the toolhead never has to swing a cantilevered arm across the plate, so tall vertical walls on a helmet stay straight as the layer stacks.
Speed is the second argument. A 700mm/s rating with 40000 mm/s^2 acceleration and a 50mm^3/s high-flow hotend is not just a spec-sheet number on a multi-day helmet. Higher acceleration with a rigid CoreXY frame means the short, thick perimeters on armor walls resolve cleanly, and the print finishes in fewer days, which is what actually matters when a convention date is fixed and immovable. The 300C hotend covers PLA, PETG, ABS, ASA, PA and PC plus carbon-filled variants, so material choice stays open to you.
Setup is the least glamorous but most valuable feature. The eddy current scanning sensor with pressure-sensing touch points replaces manual leveling, and on a plate this size that saves a lot of frustration. A dial-in test on a 500mm square takes real time with a paper test, and getting it wrong costs you a full plate of filament. The 1280×720 HD camera with Obico integration lets me check a print from another room, which is how I catch a first-layer failure early rather than after.
The honest weakness is the heated chamber. The interface is reserved for an optional module, so out of the box this is an open-frame machine. That is fine for PLA and PETG, which is where most cosplay work starts, but if you plan to print large ASA armor outdoors in summer you are budgeting for an extra accessory and a curing plan. Two standard 0.4mm nozzles also come with it, so plan on a 0.6mm or 0.8mm for thick armor walls, which is where your print time savings really come from.
When the SV08 MAX is the right machine
This is the printer for the build where a prop is physically larger than 350mm in one direction, or where a helmet shell is the difference between a smooth one-piece and a four-part assembly. Cosplayers doing convention-scale replicas of screen-accurate helmets, or hard-surface props like shoulder pauldrons and oversized blasters, get the most out of the extra footprint. It also pays off if you batch, because a 500mm plate holds pieces a smaller machine could only run one at a time.
That footprint cuts both ways, though. At 86.8 pounds the frame needs a solid, level table, and 28 x 27.6 x 29.5 inches of floor space is not something you tuck into a corner. Reviewers report a 64 percent five-star share against 13 percent one-star, which is normal variance for a new large-format release, so treat it as an early platform rather than a settled design.
When to pick a smaller machine instead
Choose something else if your work is mostly accessories, gauntlets, buckles, and detail parts under 300mm, because you would be paying for capability you never touch. It is also the wrong answer if you have limited bench space, if you want multi-color output out of the box, or if ABS and ASA are your primary materials and you would rather not add a chamber module separately. For enclosed multi-color work the Creality K2 Plus Combo is the more sensible machine.
2. Creality K2 Plus Combo – 16-Color Printing in a 350mm Cube
Creality K2 Plus Combo 3D Printer, Multi Color Printing with New CFS 600mm/s High-Speed Full Auto-Leveling Dual Al Camera Next-Gen Direct Drive Extruder Large Build Volume 13.78×13.78×13.78inch
350x350x350mm build volume
16-color CFS
60C heated chamber
600mm/s, 30000 mm/s^2
Pros
- CFS system gives up to 16 colors and cuts hand painting time
- 350mm cube handles large models without splitting
- 60C chamber plus 350C hardened nozzle suit ASA and PPA
- 18 smart sensors and dual AI cameras catch failures
Cons
- 17 percent one-star share shows early firmware and QC variance
- Weighs 70.4 lb so it needs a stable bench
- Chamber heating tops out at 60 C
The K2 Plus Combo is the machine I recommend to people who are tired of painting. Four CFS feeders deliver up to 16 colors with RFID filament auto-identification, and on a prop with a painted logo, a gradient cloak lining, or a set of armor plates in four different team colors, that turns a two-day hand-paint session into a slicer change. For cosplay, color work is where the real hours go, so this is the feature I look at first even when it is not the biggest cube in the room.
The 350 x 350 x 350mm build volume is the sweet spot for wearable work in my experience. It covers a chest plate, a back plate, a pair of forearm bracers, or a helmet shell without the awkward rotation you get on a smaller plate, and the dual independently motorized Z-axes with auto bed tilt handle a large flat first layer far more reliably than a single Z screw. A 600mm/s rating with 30000 mm/s^2 acceleration from FOC step-servo motors keeps throughput high on thick-wall parts.
Material handling is the quiet strength. The chamber holds up to 60 C and the hardened steel nozzle reaches 350 C, so ASA and PPA are on the table. Those two are the materials I reach for when a costume piece will be worn in a warm convention hall, carried through a car park on a hot day, or flexed repeatedly at the shoulders and elbows, and PLA is simply too soft and too heat-sensitive for that. The dual AI cameras are genuinely useful, one watching the chamber for spaghetti failures and one on the toolhead for flow tuning.
The die-cast aluminum Matrix frame is the other reason this holds accuracy at size, and 18 integrated sensors mean you get a notification instead of finding out from a photo the next morning. I would flag the rating spread honestly: 66 percent five-star against 17 percent one-star points to a platform that is still maturing, and the occasional firmware quirk is real. Budget a weekend with the machine before you start a deadline-critical build.
Where multi-color changes the workflow
If your character design relies on painted detail rather than a single monochrome shell, the CFS system removes an entire finishing step. Detail props, visor frames, trim pieces, and small armor accents can be printed in color and then only touched up with a clear coat. It also handles multi-material, so you can print a hard outer shell with a flexible inner liner in one go, which is a genuine comfort win for a mask or a gauntlet that has to sit against skin.
It also helps when you are replicating a design with strict color separation, such as a helmet with defined visor and trim colors, or a gauntlet with two-tone plating. Four filament feeders means those colors load once and stay loaded, and RFID identification means the machine knows which material is where.
Where it falls short
Two things to weigh. The 60C chamber ceiling is modest next to the 65C machines in this roundup, so the toughest engineering filaments are out of reach. And at 70.4 pounds, 16.1 x 15.4 x 18.7 inches, and a fixed 16-color setup, it is a large commitment for anyone printing mostly small parts. If you are not using the color features, a simpler single-extruder machine gives you more plate for less money.
3. Longer LK5 Pro – The Budget Route Into 300mm Printing
Longer LK5 Pro 3D Printer with Dual Z-Axis Upgrade, 4.3″ Color Touch Screen, Silent Motherboard, Large Print Size 11.8″x11.8″x15.7″, Fully Open Source, Filament Run-Out Detection
300x300x400mm build volume
180mm/s
4.3 inch color touchscreen
26.4 lb frame
Pros
- Lowest-cost route into the 300mm class of this roundup
- Tall 400mm Z suits helmets and torso pieces
- Open-source firmware and hardware invite real customization
- Lattice glass plate releases prints easily and stays flat
Cons
- No heated chamber so large ABS and ASA parts warp more readily
- 180mm/s is slow beside 600 to 700mm/s machines
- Plastic bed style construction is less rigid than all-metal frames
Budget matters in this hobby, because the printer is only one line item. You still need filament, sandpaper, filler primer, paint, and a convention ticket.
The Longer LK5 Pro is the reason we could build a complete list of parts without quietly cutting the paint budget in half. At 300 x 300 x 400mm it still clears the wearable threshold, and that 400mm Z is the detail that matters more than the headline footprint, because helmets and neck pieces stack vertically.
This machine has been on the market since September 2020, and that maturity shows in the review profile: 68 percent five-star against only 9 percent one-star across 664 ratings, which is the healthiest distribution in this roundup. Open-source firmware and hardware are a genuine feature here, not a compromise, because you can adjust settings the way your parts need rather than accepting what the factory profile gives you. The reinforced diagonal-bar triangular frame is designed to damp vibration, and the TMC2209 drivers are quiet enough to run in a shared room.
Two sensors earn their place on long jobs. Filament run-out detection and power failure detection with resume mean a 30-hour helmet does not become scrap because a spool ran dry at hour 22 or a breaker tripped. With a 4.3 inch color touchscreen and 90 percent pre-assembly, the setup is approachable, and the lattice glass plate makes part removal far easier than peeling off a textured PEI sheet, which matters when you have a big curved shell to release.
Now the part I always say out loud: there is no heated chamber. That means ABS and ASA on a large plate will curl at the corners unless you brace the part or seal the printer. For most cosplay work, PLA and PETG solve the problem instead. PETG in particular is what I use for wearable armor on this machine, because it is tougher than PLA and softer than ABS, so it survives being dropped in a costume trailer.
What this printer is genuinely good at
It handles a helmet, a chest plate, a back plate, or a set of limb armor in a single session, and the tall build volume means tall parts do not need to be rotated to fit. It suits a cosplayer who is printing constantly and wants predictable results, since the sensor suite and the long production history reduce the chance of a surprise failure. It is also the easiest machine here to modify, so if you later want a heated chamber or a different hotend, the open platform accepts it.
The math works in your favor here. A slower machine finishing a job on day two instead of day one is a problem when you have three weeks, and a non-problem when you have two months. Long print times only hurt when a convention deadline is closing, and with sensors that pause and resume, a slow machine is a much lower risk than a fast one running unattended for days.
Where you will feel the limits
180mm/s is a long way behind the 600 to 700mm/s machines in this roundup, and on a heavily detailed helmet you will feel it in hours, not minutes. The open frame also means no filtration, so ABS and PPS-CF style materials are unpleasant to run in a bedroom or a small apartment. If your calendar is tight, or if heat-resistant materials are central to the build, move up to an enclosed machine instead.
4. Creality K2 Pro Combo – Multi-Color Workhorse in a 300mm Cube
Creality K2 Pro Combo (A) 3D Printer, Multicolor Color Printing with CFS, 600mm/s High-Speed, Dual AI Camera, Active Chamber Heating, Auto Leveling, Large Build Volume 300×300×300mm
300x300x300mm build volume
CFS 16-color
60C active chamber
600mm/s
Pros
- CFS 16-color system bundled in the package reduces painting time
- 300mm cube is a true large-format fit for helmets and armor
- 600mm/s plus 20000 mm/s^2 acceleration keeps throughput high
- Nozzle AI camera auto-tunes flow in real time
Cons
- 300mm cube is smaller than the 350 to 500mm machines
- 17 percent one-star share points to QC and software immaturity
- Chamber capped at 60 C limits harder engineering filaments
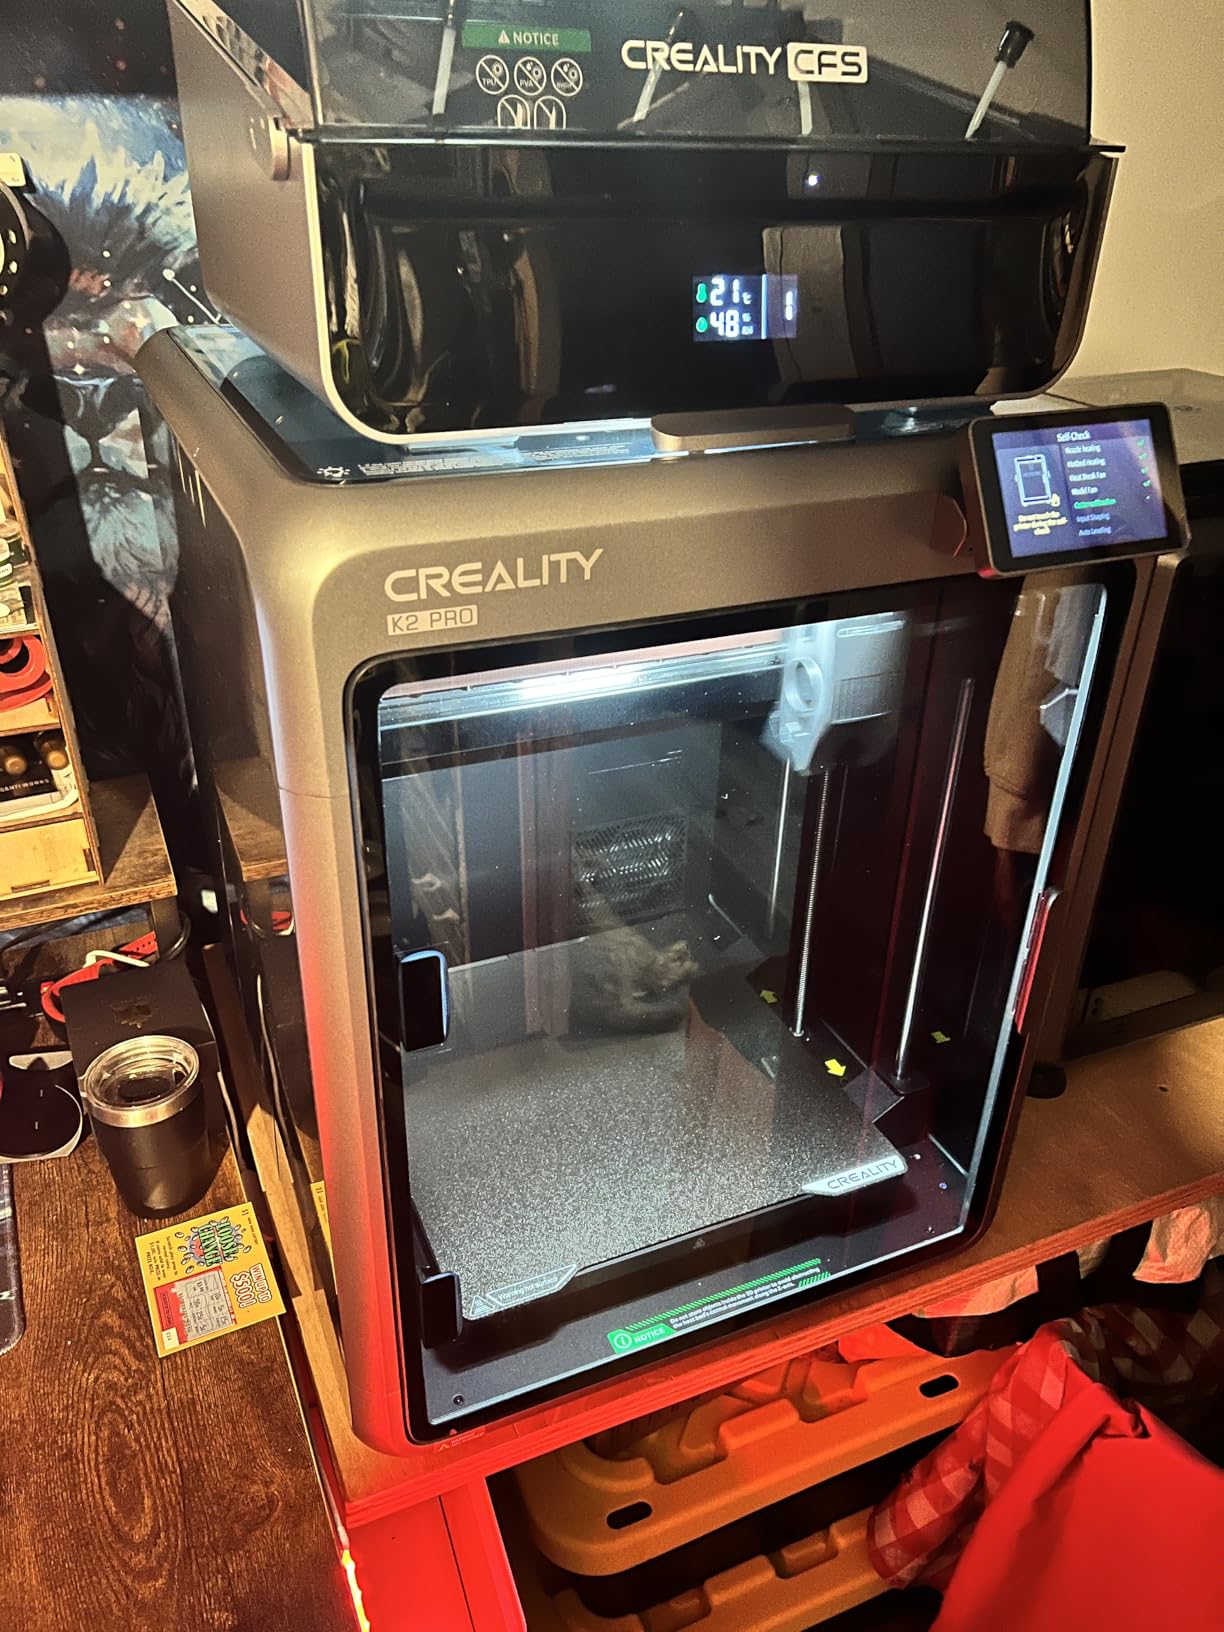
The K2 Pro Combo is the same idea as the K2 Plus, scaled to a 300mm cube, and for a lot of cosplay builds that difference is the whole decision. A 300 x 300 x 300mm plate is enough for most helmets, most forearm and shin armor, and a chest plate laid at a sensible angle. The 600mm/s rating and 20000 mm/s^2 acceleration from FOC step-servo motors on linear rails mean you are not trading speed for the color system, which is where many multi-color machines usually disappoint.
Active chamber heating to 60 C reduces corner warp on ASA and PPA, and the direct-drive extruder with hardened steel gears moves 40mm^3/s through a quick-swap hotend. That flow rate is plenty for a 0.6mm nozzle on a cosplay profile, which is the nozzle I recommend for armor walls. Area-probing bed leveling is a nice bit of engineering: it checks only the model area rather than sweeping a mesh across the whole plate, so setup is quick even on a large surface.
The two cameras do different jobs and both are useful. The chamber camera monitors the build and catches a failed first layer or a spaghetti event. The nozzle camera watches extrusion in real time, auto-tuning flow rate and detecting a waste chute blockage, which is a genuine saver on a long 16-color job. Wi-Fi and LAN with OTA updates means you can start a print from your phone and watch it from a convention prep room.
The rating spread is the thing to plan around: 65 percent five-star against 17 percent one-star. Owners love the pairing of bundled CFS plus an enclosed heated chamber, and the complaints cluster around software maturity and hardware variance. I would run a few calibration parts before a deadline build, and keep an eye on the Creality OS updates, since several of the rough edges in early reviews have been software-side.
Best fit for costume builders
Pick this when you want color without a separate single extruder machine, and your parts fit inside 300mm. Detail work on a character with strong color blocking, small props, and accessories print faster in color here than painted by hand. The hardened steel extruder and quick-swap hotend also make it a better machine for anyone who will be running carbon-filled PETG or similar abrasive material alongside standard filament.
It is also a good batching machine, since a 300mm plate can hold many small cosplay parts at once, and faster speeds make those batch jobs less painful. For anyone producing gifts, prop replicas for a group, or a convention suite of matching pieces, that throughput matters more than the last 50mm of build volume.
Where the 300mm cube bites
If your design includes a one-piece full torso shell or an oversized prop, you will be splitting the model again, which reintroduces every seam problem this roundup exists to solve. The 60C chamber ceiling is also a limitation if you plan to print engineering-grade material. And with four additional filament feeders in play, a print that fails costs you far more material than it would on a single-extruder machine.
5. QIDI PLUS4 – Built for ABS, ASA and PA Armor Shells
QIDI PLUS4 3D Printer, 65℃ Chamber Heating, 370°C Integrated Nozzle
300mm-class build volume
65C actively heated chamber
370C integrated nozzle
59.4 lb frame
Pros
- 370C integrated metal nozzle and 65C chamber handle PPS-CF and PPA-CF
- Second-generation 400W chamber heating cuts warp on big ABS and ASA parts
- Dual motor Z-axis with 10mm shafts and a 6mm bed holds flatness
- About ten minutes from unboxing to first print
Cons
- Multi-color requires the separately sold QIDI BOX
- Real learning curve for first-time operators
- Occasional filament feed and nozzle maintenance needs manual cleanup
The QIDI PLUS4 is the machine I trust when the material choice is non-negotiable. The 80W high-temperature hotend with a multi-metal integrated throat reaches 370 C, and the second-generation 400W active chamber heating circulates air behind dual-layer insulation to keep the whole box at a steady 65 C. That combination is what makes large ABS, ASA, PC and PA parts come off the bed flat instead of lifting at the corners, and corner lift is the single most common cause of a failed large print.
At roughly 300 x 300 x 280mm, the build volume is 12 x 12 x 11 inches, which is enough for a helmet, a chest plate, or a batch of limb pieces. The heavy part of the design is the Z hardware: independent dual motor-driven axes on 10mm linear shafts and lead screws, feeding a 6mm thickened aluminum platform. On a tall print like a helmet, that is the difference between a smooth vertical wall and a slightly leaning, visibly stepped one that shows through the paint.
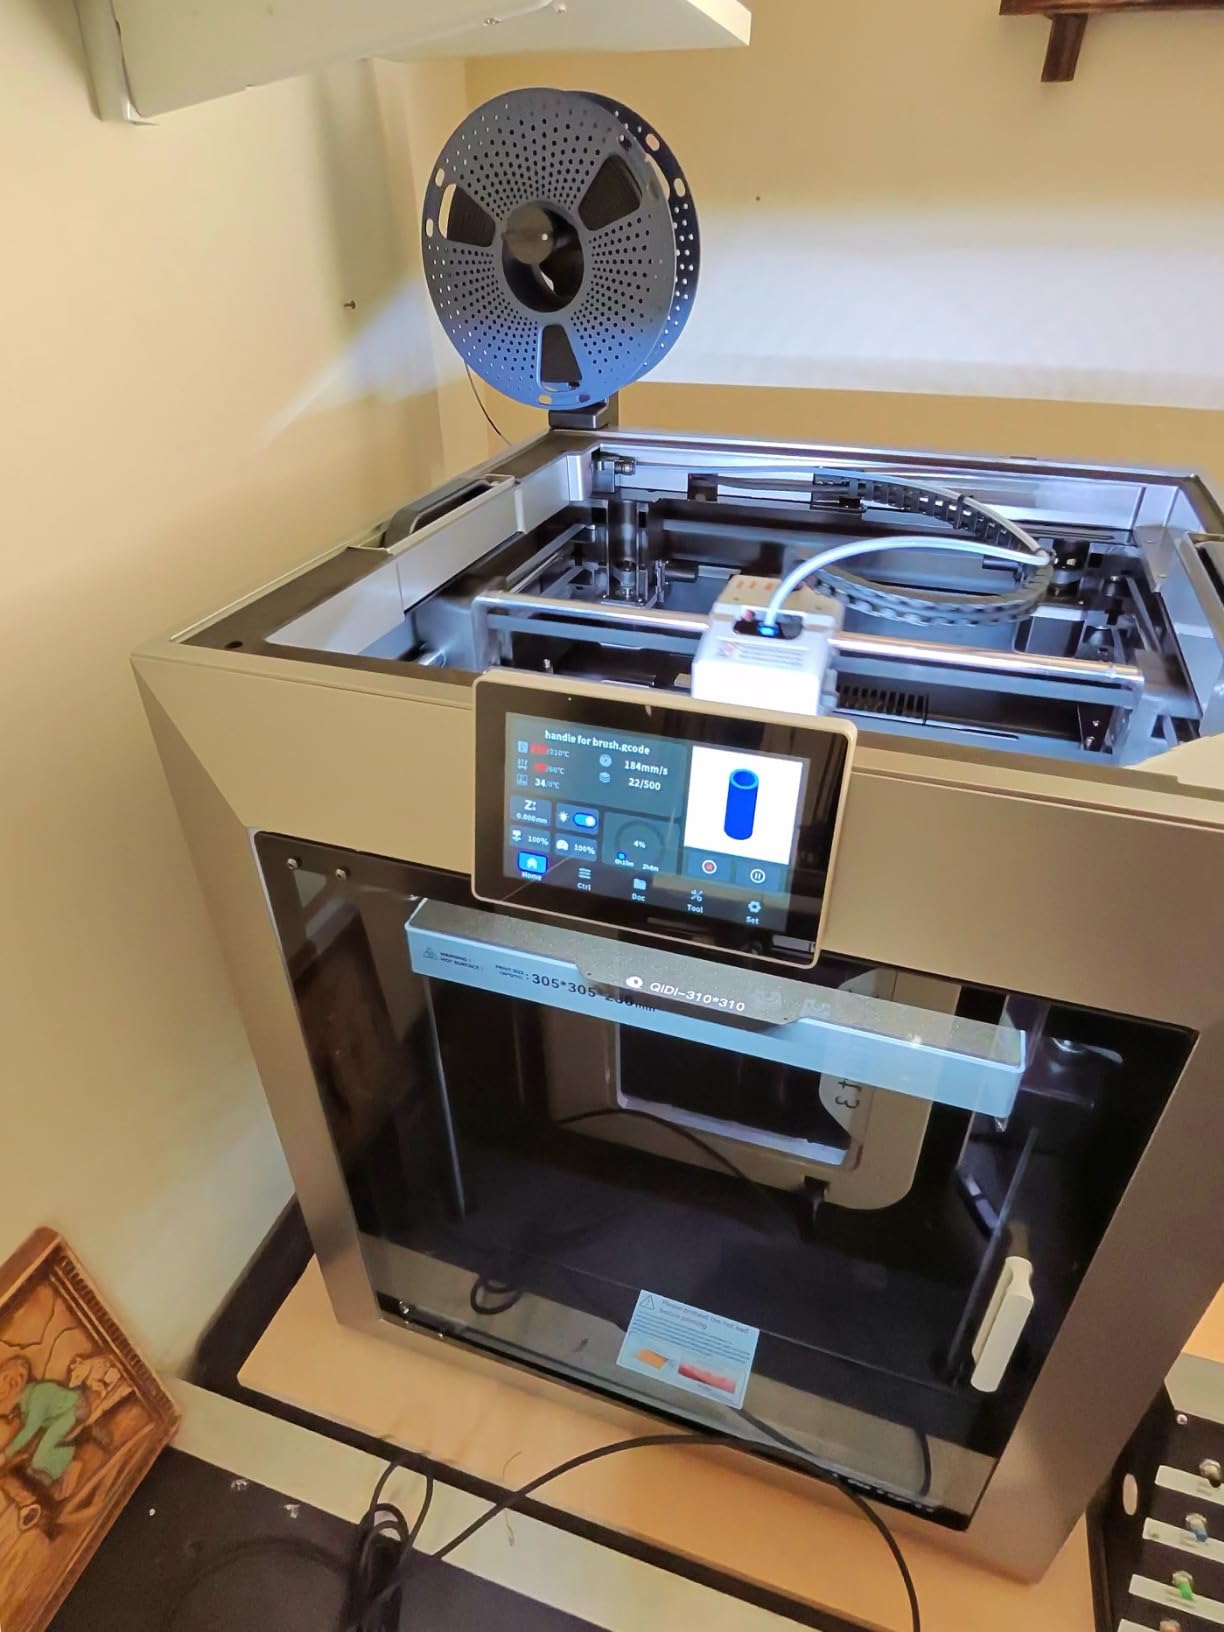
Setup time is genuinely short. Owners consistently report being unboxed and printing in about ten minutes, and that matters when the printer itself was a weekend project. The HD camera with remote monitoring and time-lapse is there for the same reason it is on every other machine in this roundup, a long ASA armor job will run overnight and you need to be able to see it. Filament wrap and break detection reduce waste, and QIDI Studio plus the mobile app handle remote printing.
There is an integrated filament cutter, which means the machine is ready for multi-color expansion through the QIDI BOX, but that box is not included. That is the main gap, and it is worth knowing before you plan a color-heavy build. The other honest note is that this is not a beginner machine; the learning curve is real, and reviewers mention occasional filament feed and nozzle maintenance that needs hands-on cleanup.
When material choice decides the printer
Choose the PLUS4 if your character design calls for heat deflection resistance, a rigid finish that holds a curve, or a material that has to survive a hot convention hall. ABS and ASA are the classics, and with a 65C chamber they print large and flat on this machine in a way that open-frame printers cannot match. For a costume you will wear all weekend in an un air-conditioned hall, ASA is the material I would choose, and this is the machine that prints it well.
It also makes sense as a companion to a smaller printer, since the small machine handles detail props and this one takes the shells. And if you are still learning the craft, the fast setup and responsive QIDI support mean you are not blocked waiting on help when something goes wrong at hour 20 of a build.
Where it is not the answer
Skip it if color is central to your build, since multi-color is an add-on purchase. It is also a heavy machine at 59.4 pounds and 19.29 x 20.07 x 22.24 inches, so plan the bench before it arrives. And if your parts are all under 200mm, a 300mm-class volume is money you do not need to spend.
6. FLASHFORGE Creator 5 Pro – Four Toolheads for Multi-Material Armor
FLASHFORGE Creator 5 Pro 4-Toolhead 3D Printer, Industrial Multi-Material & Color Printing, 65°C Active Heated Chamber, Near-Zero Waste System, CoreXY 600mm/s Printing
4 independent toolheads
Enclosed 65C heated chamber
600mm/s CoreXY
39 lb frame
Pros
- Four toolheads with no-purge FlashSwap changes handle complex multi-material builds
- Near-zero waste system cuts purge filament and speeds multi-color runs
- 65C enclosed chamber supports ABS PC and PA
- HEPA 13 plus carbon filtration makes indoor high-temp printing practical
Cons
- Only 131 reviews so far so long-term reliability is unproven
- Four toolheads add cost and complexity versus a single extruder
- Multi-toolhead servicing takes more upkeep
Four independent toolheads is a genuinely different proposition from the CFS systems elsewhere in this roundup, and it is the reason this machine is here. A filament changer system swaps one material for another, so any print still needs purging between colors. Four separate toolheads means each material is already loaded and ready, so a prop with a hard shell, a flexible trim, a translucent visor element and a metallic detail accent can be printed without the wipe towers and purge waste that single-extruder color changes generate. The 7-second FlashSwap changer reinforces that.
The second thing I appreciate is the enclosure and the heat. A fully enclosed frame with active chamber heating up to 65 C keeps ABS, PC and PA parts dimensionally stable across a long print, and the ultra-rigid integrated CoreXY architecture on linear rails with 1.5GT high-torque belts holds accuracy at the 600mm/s speed rating. The 66 percent five-star share is strong for a machine that only became available in August 2026.
The filtration is a sleeper feature for cosplay. Dual HEPA 13 plus activated carbon with continuous airflow means ultrafine particles and fumes from engineering filament are actually captured, which changes where you can put the printer. A garage or a workshop with a window is workable, and a bedroom is not. For anyone printing ABS and PC in an apartment, that is a real constraint removed rather than a line on a spec sheet.
Calibration is automated too, with toolhead offset calibration, vibration compensation and dynamic flow calibration handled by the machine, plus a built-in HD chamber camera that produces time-lapse automatically. Flash Studio runs on desktop or mobile for remote control. The trade-off is complexity: four toolheads means more to maintain, and the review base of 131 ratings is too small to tell you how this holds up over three years.
Why four toolheads change a cosplay build
The use case is a costume built from more than one material, which is more common than people expect. A helmet with a rigid outer shell and a flexible inner comfort liner, gauntlets with a rigid plate over a flexible glove mount, or a prop with a translucent lens set into an opaque body are all single-print jobs here rather than four separate jobs. Because each material stays loaded, you also avoid reloading filament on a 20-hour build, and a near-zero waste system cuts the purge material you would otherwise throw away.
It also scales. If you are producing matching pieces for a group, the four toolheads let you set up a material lineup once and then run print after print without babysitting swaps. For advanced builders doing multi-color and multi-material work, that throughput is the argument.
Where four toolheads are overkill
If your parts are a single material in a single color, this machine solves a problem you do not have, and you pay for that in both expense and maintenance time. Four toolheads also mean four nozzles to keep clean, which is real work with abrasive or filled filament. And with 131 reviews, there is not yet the long-term evidence that cosplayers buying a multi-year machine usually want.
7. Creality Ender 5 Max – 400mm Cube for One-Piece Helmets
Creality Ender 5 Max 3D Printer 400×400×400mm Large Build Volume, 700mm/s Fast Printing Speed, 64-Point Auto Leveling, All-Metal Frame & Dual Gear Extruder, Multi-Printer Control Over WLAN
400x400x400mm build volume
700mm/s CoreXY
64-point auto leveling
All-metal die-cast frame
Pros
- 400mm cube prints full-size helmets and armor shells in one piece
- Die-cast all-metal frame and X-axis linear rail hold accuracy on tall prints
- 64-point auto leveling plus auto Z-offset suits first-time owners
- Direct-drive hardened dual gear extruder built for long runs
Cons
- No enclosure included so ASA and ABS work is harder
- No multi-color without add-on hardware
- 1000W bed is reported to be slow to reach 80 C
This is the build volume question answered plainly. A 400 x 400 x 400mm cube means a full-size helmet shell goes down in one piece, at any orientation, without slicing it into quarters. If seam lines are the thing you most want to avoid on a helmet, this is the machine that removes them without an upgrade path or a compromise. It is also a batching platform, since a 400mm plate holds several armor pieces in one session.
The frame is where the money went. A reinforced die-cast aluminum all-metal frame with a precision linear rail on the X axis is what keeps a tall, heavy print from ringing, and the 700mm/s CoreXY rating with high-torque motors is backed by that rigidity rather than by acceleration alone. For cosplay specifically, that accuracy shows up on the vertical walls of a helmet and on the long straight edges of a chest plate, which are exactly the surfaces that show defects through primer and paint.
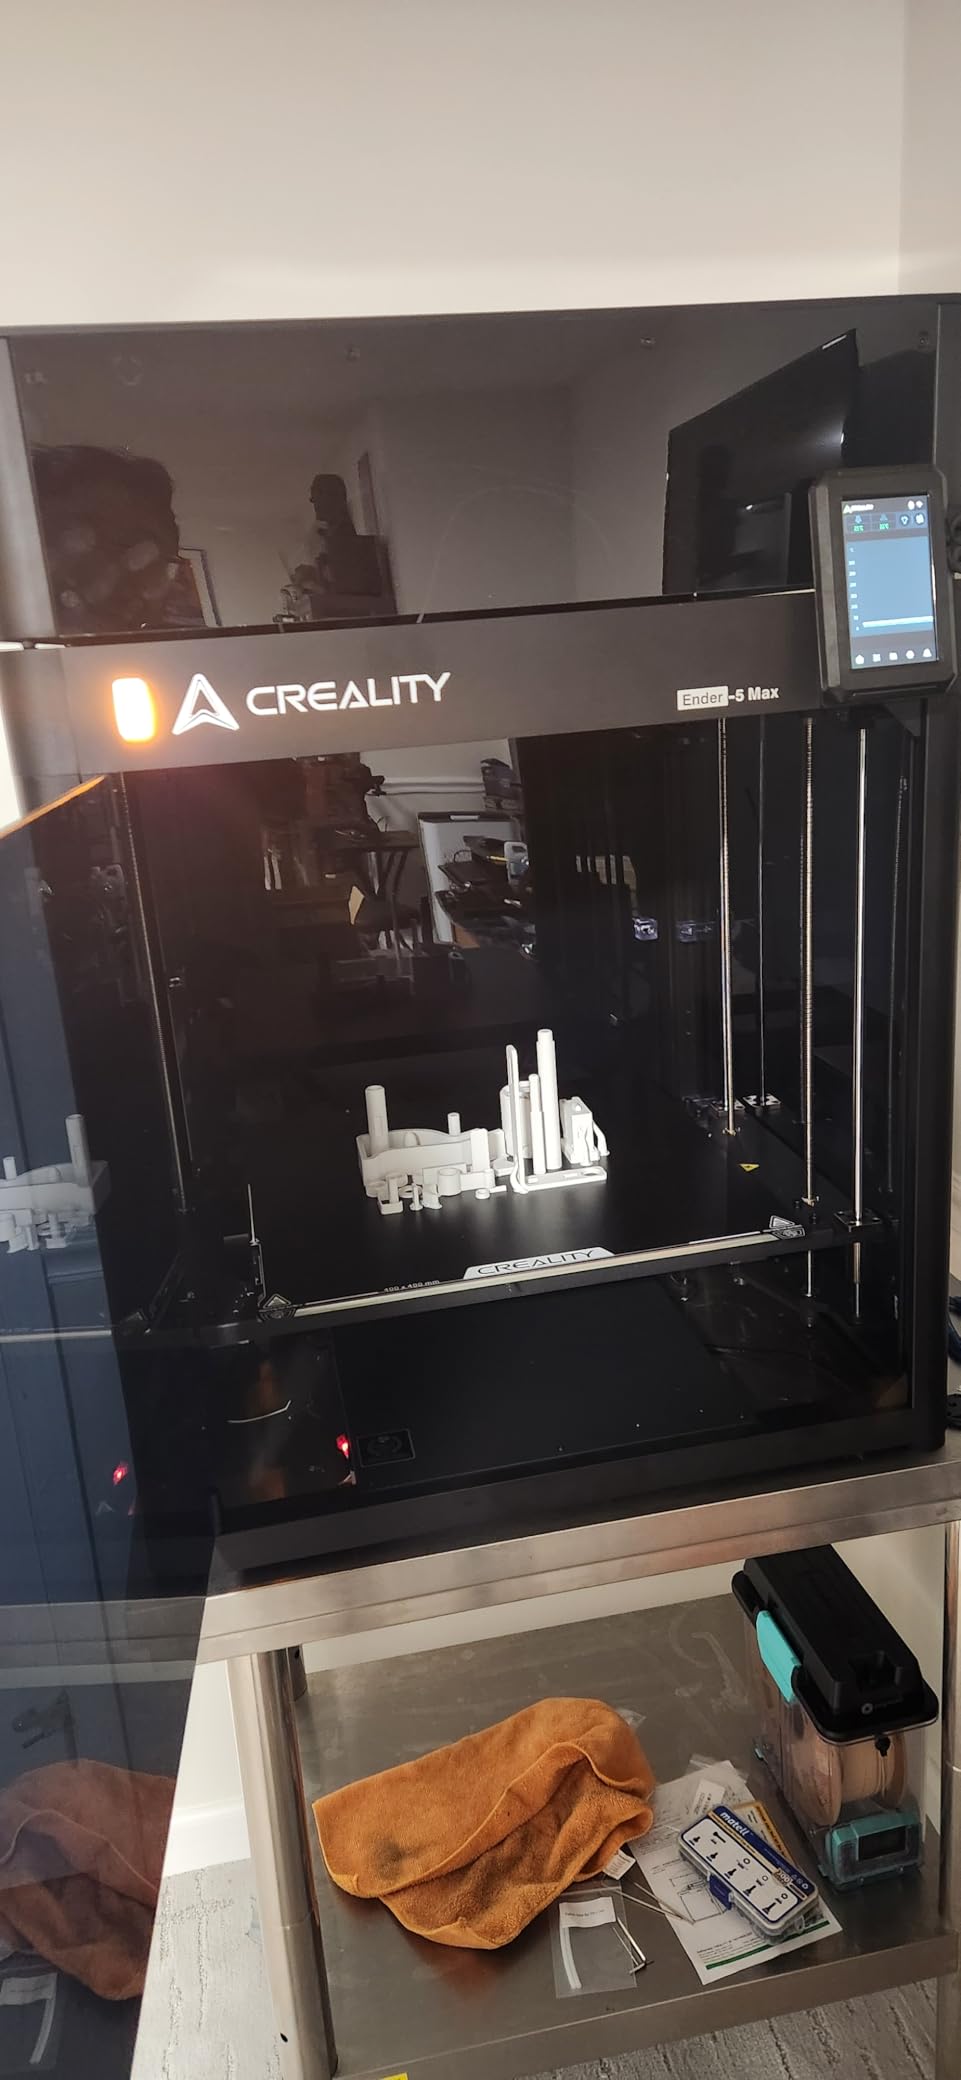
Automation is thorough for a first machine. 64-point automatic leveling plus auto Z-offset handles the part of setup that normally causes failures, and the direct-drive hardened dual gear extruder is built for sustained production rather than occasional use. WLAN multi-printer control with grouped management and a tri-color status indicator is genuinely useful if you ever run more than one machine, which many builders with tight deadlines do. Owners report reliable results across PLA+, PETG, PETG-CF, ASA, ABS and HT-PLA.
The reviews are genuinely split, and you should know why. Some owners call it a dependable workhorse that handles huge single-color engineering and cosplay helmet prints without a problem. Others report vibration and loosened fasteners on early units, warped beds, slow bed heat-up, and AI failure detection that is inconsistent. The 1000W bed takes a long time to reach 80 C according to multiple owners, so plan warm-up time into your schedule.
Where the 400mm cube pays off
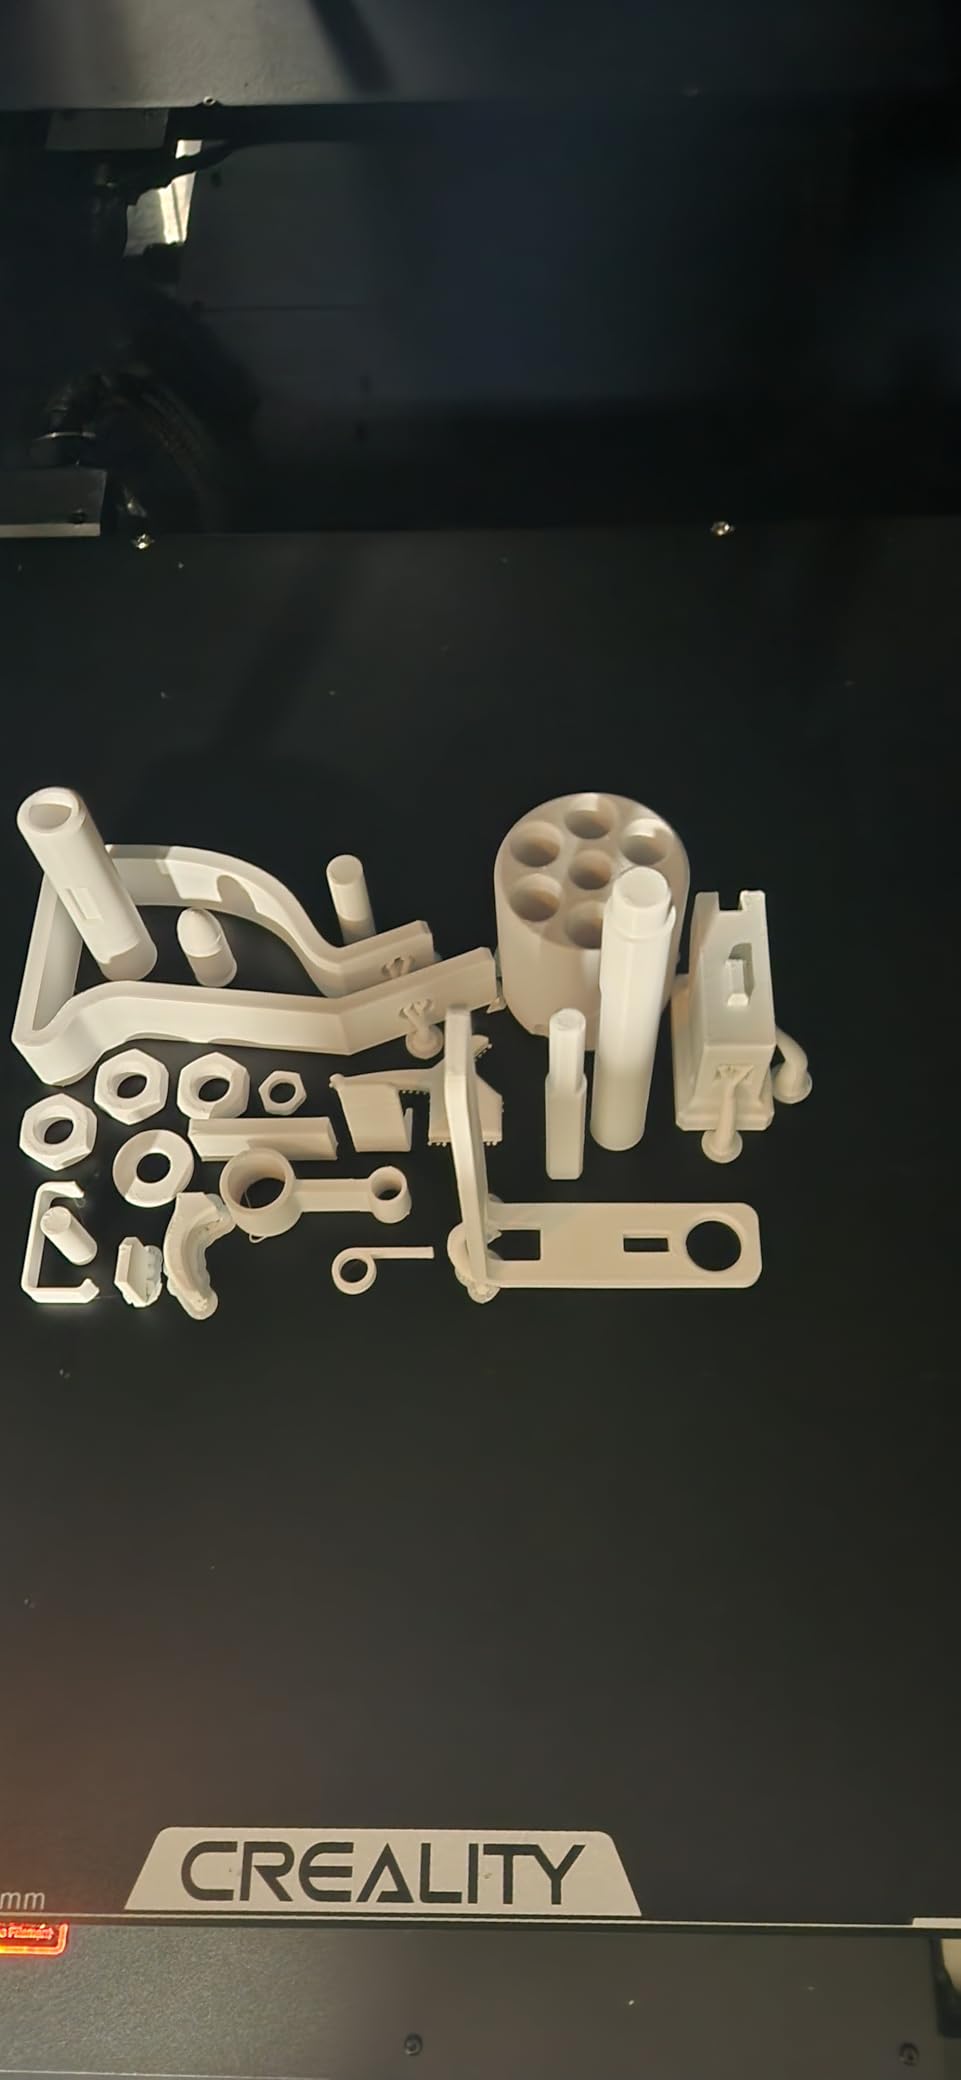
Full helmets, oversized pauldron and knee armor, wide chest and back plates, and large props are all jobs that force a split on a 300mm machine. At 400mm they are not. For cosplayers replicating full-size screen props, this is the practical sweet spot: big enough to stop splitting, and smaller and lighter to manage than a 500mm cube. Owners specifically cite helmet printing as the standout use.
It is also a good batch machine for a suite of matching pieces, and the auto leveling means a beginner can get a reliable first layer on a plate this large, which is normally the hardest part of scaling up. If your workflow is single-color, single-material printing of large shells, that is exactly what this machine is built to do.
Where it falls down
No enclosure is the headline limitation, and many owners add one separately. Without a chamber, large ABS and ASA parts warp more readily, and a warped 400mm plate is a lot of filament to lose. Multi-color is not available without add-on hardware, and the assembly of a flat-packed machine this heavy realistically needs two people. If you need color or heat-resistant materials out of the box, look at the K2 Pro or a heated-chamber model instead.
8. QIDI Max4 Combo – Highest Rated, 390mm Heated-Chamber Build
QIDI Max4 Combo 3D Printer, 390×390×340mm Build Volume, 65℃ Heated Chamber
390x390x340mm build volume
65C heated chamber
800mm/s
120 lb frame
Pros
- 390x390x340mm volume fits full-size cosplay helmets on one plate
- Highest average rating in this roundup at 4.4 with 77 percent five-star
- 800mm/s with closed-loop motors and 30000 mm/s^2 acceleration
- Full-surface silicone bed holds a flat first layer and resists warp
Cons
- Polar Cooler must be purchased separately
- 120 lb and 28x28x30 in needs a purpose-built heavy table
- Some QIDI BOX sync issues reported
- Documentation is sparse for a machine this complex
The Max4 Combo has the strongest owner feedback of any machine here. At 4.4 average with 77 percent five-star and 9 percent one-star across 30 detailed reviews, this is the highest-rated printer in the roundup, and the reviews are unusually specific about cosplay work: full-size helmet prints, Iron Man and Doctor Doom suit shells, minimal calibration on first power-up, and flat beds that held up over heavy multi-month filament use with no clogs.
On paper it is among the most complete machines in the group. The 390 x 390 x 340mm build area is 55 percent larger than the MAX3 before it, closed-loop motors on X and Y reach 800mm/s with 30000 mm/s^2 acceleration, and the 2mm lead screw with an anti-backlash nut on Z reduces the vertical gaps that show up as a visible seam in a tall helmet print. The full-surface silicone heated bed is the quiet hero, since even heat distribution across a 390mm plate is what produces a flat first layer and resists warping.
Heat handling is complete: a 65C active chamber plus a 40mm^3/s high-flow hardened steel hotend covers ABS, PC, PPS-CF and CF-reinforced nylon. A built-in AI camera detects abnormalities such as a spaghetti failure and pauses the print on its own, which on a long build is worth a great deal. A large touch screen, and QIDI support that owners repeatedly describe as fast and effective, round it out.
Be clear-eyed about the size. At 120 pounds and 28 x 28 x 30 inches, this is not a machine you set up on a desk. The Polar Cooler is sold separately, which is the main reason the full ABS-CF and PC capability costs more than the headline suggests. Some owners report QIDI BOX sync issues selecting the wrong filament, and documentation is sparse for a machine this complex, so keep notes as you learn it.
Best fit for experienced builders
Pick the Max4 if you are printing near-continuously and your parts are large, heated, or both. A 390mm plate covers a full-size helmet in one print, and the 65C chamber means you are not fighting warping on ASA or PC. Owners cite QIDI support as a genuine advantage, which is worth more than any spec when a build is on a deadline and something fails at hour 40.
Multi-color is available through the QIDI BOX expansion for 16 colors with filament level monitoring, so if your design needs color you can grow into it, though the reviews suggest testing the sync carefully first. The silicone bed is also the choice I would make for a big flat chest plate, because first-layer consistency across a large area is what prevents the cupping you fight with braces otherwise.
Where the size and price are hard to justify
This is the heaviest machine in the roundup by a wide margin, and if you are printing a handful of small props a year, none of that structure helps you. The Polar Cooler add-on and a purpose-built table are real costs beyond the machine. With only 30 reviews it also has the thinnest evidence base here, so if you want a proven long-term track record over the best owner sentiment, the longer-running Creality and QIDI models have more of it.
How Big a Printer Do You Actually Need?
Start from the largest single part in your design, not from the whole costume. Measure the widest point and the tallest point of one piece, because a part only needs to fit in one orientation. Most adult heads are roughly 200mm front to back and 230mm across, which is why the 256mm class keeps showing up as too tight. A 300mm cube fits nearly every wearable piece on its own, which is the reason this roundup starts there rather than at 220mm.
Beyond that, think about which direction your parts are large. A chest plate is wide and shallow, so X and Y matter. A helmet, a boot, or a tall greave is long in Z, so a tall build axis saves you from rotating the model and dealing with a support scar. The Longer LK5 Pro at 300 x 300 x 400mm and the Creality Ender 5 Max at 400mm on all three axes both handle these differently, and the right choice depends on your character’s proportions.
Ask one more question: how many parts must come off a single plate before you want to start the next batch. Bigger plates mean fewer changeovers and less idle time, which matters most when you are working to a convention deadline. If you are comparing the best large format 3d printers for cosplay props on volume alone, the SV08 MAX at 500mm wins. If value per usable plate is the goal, 300 to 350mm is where most builds actually land, and our large format printer guide covers the wider category if you want more context.
FDM or Resin for Cosplay?
For wearable armor, FDM wins, and it is not close. A filament print gives you a tough, slightly flexible shell that tolerates being dropped, bumped in a crowded convention hall, and flexed at the shoulders. Resin produces beautiful detail, but cured resin is brittle, and a brittle wearable part fails at the thinnest cross-section, which is usually a visor edge, a strap anchor, or the tip of a horn. Most builders land on a split approach: filament for the shell, resin for small detail props and accessories. Our resin roundup for cosplay covers the detail side if you want to add a second machine.
The reasons to still consider resin are surface finish and fine features. A resin print needs far less sanding and filler to look smooth, and characters with textured fabric, chainmail, or engraved surface detail come out dramatically better. The costs are real, though: resin handling requires gloves, ventilation, and careful disposal, and the post-processing chain of washing, curing, and support removal is longer than a filament print. For a shell you wear on your head for two days, filament remains the sensible default.
Which Filament to Print Armor In
PLA is the starting point for most pieces, because it prints cleanly with minimal warping, sands beautifully, and takes paint and primer without complaint. Its weakness is heat. A chest plate in PLA in a warm hall or under stage lighting will soften, and repeated flexing at the shoulder or elbow will eventually crack it. Use PLA for props, display pieces, and anything that will be handled but not worn for hours.
PETG is the answer for wearable armor, and it is what I use on the majority of shells. It is tougher and more flexible than PLA, tolerates heat far better, and still sands and primes well. The trade-off is stringing and a slightly glossier surface that needs a little more work before paint, and it wants a slower print with good bed adhesion because it likes to lift. A brim on large flat plates is close to mandatory.
ABS and ASA are for the parts that face real heat, and they need a printer that can help them. ASA is better outdoors because UV and weather resistance come standard, and ABS is the easier of the two to print but weaker in sunlight. Both warp on large plates without a heated chamber, which is exactly what the QIDI PLUS4, the QIDI Max4, and the K2 models solve. For a costume worn outdoors in summer, ASA on a heated-chamber machine is the correct answer, not a compromise.
Print Settings by Part Type
For a helmet, print at 0.2 to 0.24mm layer height with a 0.6mm nozzle and three or four perimeters. Helmet shells need surface quality above all else, since the whole shape is visible, and a 0.6mm nozzle gets you there without a 40-hour print. Use 15 to 20 percent infill because the shell needs stiffness rather than weight savings, and prefer tree supports on curved inner surfaces so the support scar lands somewhere you were going to sand anyway.
For flat armor plates such as chest, back, and thigh pieces, layer height matters less than wall count. Run 0.28 to 0.32mm layers, four to six perimeters, and 10 to 15 percent infill, with gyroid or lightning infill if you want a stiffer result at lower weight. Brace the corners of large plates, print with the panel face on the bed rather than standing up, and keep the part flat for as many layers as the geometry allows. Corner warp is a chamber problem, not a settings problem.
For weapons, staffs, and large props, speed is the priority. A 0.8mm nozzle at 0.4 to 0.48mm layers with two or three perimeters and 10 percent infill will move a big prop far faster than a fine-layer profile, and the surface is going to be sanded and painted anyway. Thick walls, generous tab settings, and a printed handle grip area will survive convention handling far better than a fine, thin-walled prop printed at maximum resolution.
Whatever the part, slow the first layer, keep the nozzle hot and the bed textured, and watch the first three layers before you walk away. Long prints fail at the start far more often than at the end, and most of the 20-plus hour failures we have seen were first-layer adhesion problems that were visible at minute four.
From File to Convention: Slicer, Supports and Finishing
File sources are rarely the bottleneck. Public repositories such as Thingiverse, Printables, MyMiniFactory, and Cults3D hold large collections of cosplay STLs, ranging from fan-made helmet designs to community-tested armor files, and STL remains the most common format you will find. Before you commit to a file, check the reported print size and the review count, and look for a design that has been printed at full scale rather than a scaled preview render.
Slicing is where you save hours. In your slicer of choice, whether that is PrusaSlicer, OrcaSlicer, Bambu Studio, Cura, or the QIDI and Creality software bundled with those machines, set the wall count, infill, and layer height from the settings above, enable tree supports for shells, and add a brim for anything with a large flat footprint. Rotate the model so the fewest faces touch the bed, because every contact face is a sanding job later. Where you can, split a model at a natural seam line so the join disappears under a trim piece or strap.
Post-processing follows a predictable order: remove supports, sand through progressively finer grits, fill remaining layer lines with filler primer, sand again, then prime, then paint. The wall count you chose in the slicer determines how much sanding you are doing, which is the quiet argument for thicker walls on parts you will handle all weekend. If you want a broader view of filament and finishing choices before you start, our FDM cosplay guide walks through the whole process end to end.
Plan backward from the convention. Twelve weeks out, choose and test your filament. Eight weeks out, print and finish one test piece at final scale. Six weeks out, commit to the main shells. Two weeks out, print accessories and props. One week out, fit, adjust straps, and paint touch-ups only. The most common cosplay printing failure we see is not a failed print, it is a first full print started three weeks before the event with no time left for a second attempt.
One safety note worth including: keep the printer on a non-flammable surface, away from fabric and storage boxes, and do not run high-temperature material unattended overnight without a smoke alarm nearby. A printer failure that starts a fire ruins far more than a convention costume. If you add resin to the workflow later, add gloves, a wash and cure station, and ventilation at the same time.
Frequently Asked Questions
How big of a 3D printer do I need for cosplay helmets?
A 300mm-class build volume is the practical starting point. Most adult helmet shells measure under 250mm in every direction, so a 300 x 300 x 300mm printer prints them in one piece without splitting. A 400mm cube is worth the extra cost when you also build oversized props, wide chest plates, or want to batch several parts per plate.
Is PLA good enough for cosplay armor?
Yes, for props, display pieces, and anything worn briefly. PLA prints cleanly, sands well, and primes easily, but it softens in heat and can crack after repeated flexing. For a chest plate, helmet, or gauntlet you will wear for a full convention weekend, PETG is the safer material because it is tougher and far more heat tolerant.
Is FDM or resin better for cosplay?
FDM is better for wearable armor, because a filament shell is tough and slightly flexible, while cured resin is brittle and fails at thin cross-sections. Resin is better for small detail props, accessories, and surface finish, since it needs far less sanding. Most builders run both: a large format FDM machine for shells and a resin printer for detail pieces.
What nozzle size should I use for cosplay prints?
A 0.6mm nozzle is the standard choice for armor. It produces thicker walls that are stronger and faster to print than a 0.4mm nozzle, and the surface is still fine after sanding and priming. Use 0.4mm for detail props and visors, and 0.8mm for large weapons and staffs where speed matters more than surface quality.
Do I need a heated chamber for ABS and ASA armor?
For small parts, not strictly. For large flat pieces, yes, a heated chamber of 60 C or above makes a real difference. ABS and ASA warp at the corners on long prints, and a heated chamber holds the whole build volume at temperature so the material stays relaxed as it lays down. An unheated printer works fine for PLA and PETG without one.
What are the biggest 3D printers available?
Among the machines in this roundup, the Sovol SV08 MAX has the largest build volume at 500 x 500 x 500mm, followed by the Creality Ender 5 Max at 400mm in all three axes and the QIDI Max4 Combo at 390 x 390 x 340mm. Build volume is the first thing to check for cosplay, because it directly determines how many seam lines your costume needs.
Which Large Format Printer Should You Buy?
If you want one answer for most cosplay builders, the Sovol SV08 MAX is the machine I would point at first. A 500mm cube covers nearly every wearable piece in one print, the 700mm/s CoreXY motion keeps multi-day jobs to a workable length, and it carries the largest review base in this roundup, which matters when you are committing real money. The Creality K2 Plus Combo is the smarter balanced buy for anyone who wants 16-color output and a 60C chamber in a 350mm cube, and it is the one I recommend when hand painting is the part of the process you dislike most.
Match the machine to your actual project and you cannot go far wrong. Take the Longer LK5 Pro if cost is the deciding factor and you are comfortable with PLA and PETG. Take the QIDI PLUS4 or QIDI Max4 Combo when heat-resistant material is non-negotiable. Take the FLASHFORGE Creator 5 Pro when one part genuinely needs four materials. Take the Creality Ender 5 Max when one-piece helmets are the whole point and you print single color.
Whichever you choose, budget for filament and finishing materials as part of the purchase, and print a full-scale test piece before you commit to a deadline. Our picks for large format printing cover the wider category if you also build display pieces beyond the costume itself.